





Product Quick Navigation
Get a Quote
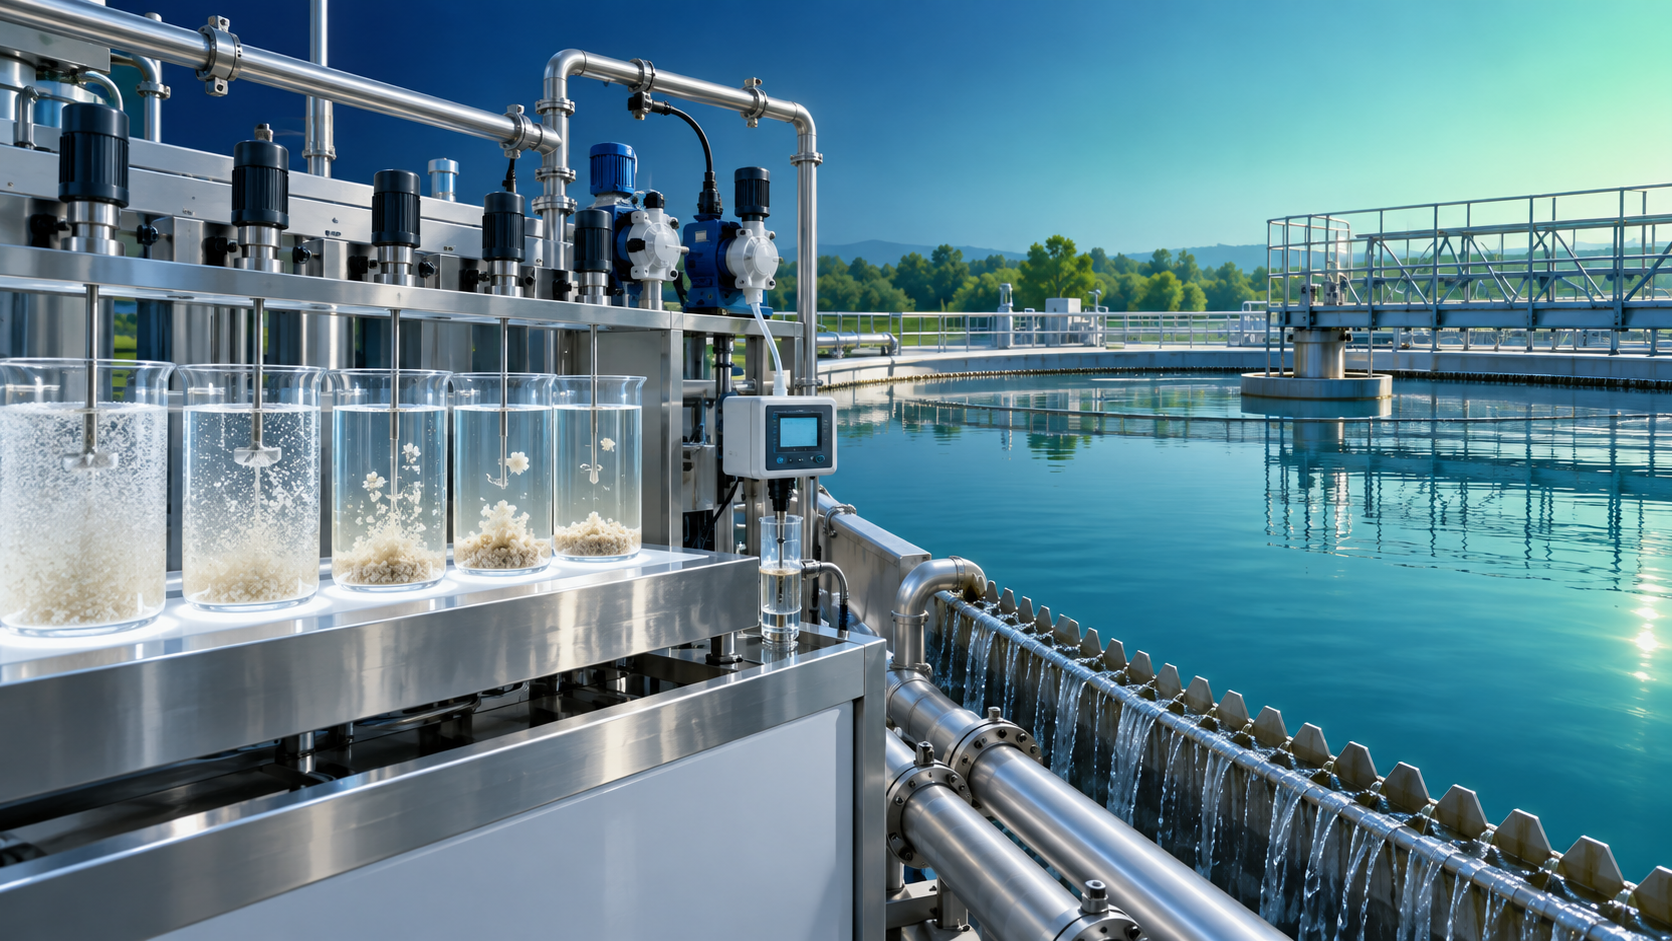
Low turbidity and low sludge production are not achieved by simply adding more coagulant. In many treatment systems, overdosing is the reason clarification becomes unstable: particle charge is reversed, flocs become weak or dispersed, filter loading increases, and sludge volume rises without a proportional improvement in water quality. The operating target is therefore not the highest coagulant dose that produces clear-looking water in a jar test, but the lowest reliable dose that meets the required treated-water quality under changing raw-water conditions.
For operators, the practical challenge is that raw water rarely remains constant. Turbidity, pH, alkalinity, temperature, organic matter, conductivity, and the type of suspended solids can change independently. A dose that worked during one shift may be inefficient several hours later. Effective control of Water Treatment Coagulants depends on recognizing which variable has changed and adjusting the process in the correct order.
Why the “more chemical, clearer water” approach fails
Coagulation works by destabilizing fine particles that would otherwise remain suspended. Clay, colloids, organic matter, metal hydroxides, microorganisms, and other fine solids often carry electrical charges that keep them apart. Aluminum- and iron-based coagulants, as well as certain polymeric products, reduce charge repulsion and create conditions in which particles can collide and form settleable flocs.
This mechanism has a limited operating window. Below the effective dose, particles remain stable and clarification is poor. Within the correct range, turbidity declines and flocs become denser. Beyond that range, excess coagulant can lead to charge reversal or create large quantities of metal hydroxide precipitate. The result may be cloudy supernatant, floating floc, high residual metal, increased filter differential pressure, or more sludge than the dewatering system can manage.
Visual clarity alone is not a sufficient control indicator. A sample can appear clear while still carrying fine particles that later break through filters. Conversely, a large, fast-settling floc can indicate a high chemical dose rather than efficient treatment. The better question is whether the selected dose produces stable settled-water turbidity, acceptable filter performance, controllable sludge characteristics, and compliance with the required treated-water specification.
Start with raw-water characterization, not a fixed feed rate
A fixed coagulant pump setting is convenient, but it assumes that the raw water has fixed chemistry. That assumption is rarely safe. Turbidity is important, but it is only one part of the dosing decision. Two water sources with the same turbidity can need very different chemical programs if one contains mineral clay and the other contains colored dissolved organic matter.
Operationally useful monitoring should include the variables that explain coagulation changes:
- Raw-water turbidity: Indicates particulate loading, but not particle type or surface chemistry.
- pH and alkalinity: Determine whether hydrolysis products form effectively and whether the process has enough buffering capacity.
- Water temperature: Affects reaction rate, viscosity, floc growth, and settling behavior.
- Color or UV absorbance where relevant: Helps identify dissolved organic material that can consume coagulant without producing easily settleable solids.
- Conductivity and source-water changes: Can signal blending changes, saline intrusion, industrial discharges, or other shifts that alter treatment response.
- Settled-water turbidity and filter trends: Show whether the dose is truly improving downstream performance.
When raw-water turbidity rises suddenly, increasing coagulant may be justified, but the increase should not be automatic or proportional to the turbidity number alone. A storm event can introduce highly reactive mineral particles that coagulate readily, while another event can bring organic-rich material that requires a different pH condition, coagulant type, or polymer aid. Treating every turbidity increase as identical is a common source of excessive chemical use.
The dose is determined in the mixing zone before it is confirmed in the clarifier
Poor results are often blamed on the coagulant when the actual problem is mixing. Coagulant must disperse rapidly throughout the incoming water before hydrolysis and particle interactions become localized. If injection occurs in a low-energy area, the chemical may form concentrated precipitates, consume alkalinity unevenly, and generate fragile floc. Increasing the dose then compounds the problem.
Rapid mixing should provide prompt and uniform distribution, while subsequent flocculation should provide enough gentle energy for particles to collide without shearing apart. These two stages require different conditions. High-energy mixing is useful immediately after injection; prolonged high shear after floc has formed is destructive.
Useful signs of a mixing problem include inconsistent floc size across the basin, visible white or rust-colored chemical precipitate, good jar-test results but poor full-scale clarification, or a need for unusually high doses to maintain settled-water quality. Before changing the chemical program, verify injection location, dilution water availability, static mixer condition, rapid-mix equipment performance, flocculator speed, and hydraulic short-circuiting.
Coagulant dilution can also matter. Some products are supplied at concentrations that are practical for transport and storage but can be difficult to distribute uniformly at very low flow rates. Controlled dilution may improve initial dispersion, although excessive dilution can create unnecessary handling volume and may affect product stability depending on the chemistry. The product supplier’s handling guidance and the plant’s actual feed equipment should be considered together.
pH and alkalinity determine whether the chemical can do its job
Many inorganic coagulants consume alkalinity as they hydrolyze. If the raw water has limited alkalinity, a dose increase may lower pH enough to weaken coagulation performance, reduce floc density, or create residual metal concerns. In that situation, adding more coagulant is not the corrective action; restoring suitable alkalinity or adjusting pH may be necessary.
The effective pH range depends on the specific coagulant and the raw-water composition. Aluminum sulfate, polyaluminum chloride, ferric chloride, ferric sulfate, and blended products do not behave identically. A coagulant selected for a broad operating range may still perform poorly if the actual process pH moves outside its useful window or if dissolved organic matter changes the reaction pathway.
Routine pH readings should be interpreted at more than one point. Raw-water pH shows the incoming condition, but the pH after rapid mixing and after clarification reveals whether chemical addition is shifting the process beyond a stable range. A plant that monitors only raw-water pH can miss the local chemical effect that governs floc formation.
Alkalinity addition also has trade-offs. Lime, sodium hydroxide, sodium bicarbonate, or other conditioning chemicals may restore process stability, but each changes operating costs, solids production, scaling potential, and handling requirements. The goal is not to maximize alkalinity; it is to maintain the chemical environment needed for reliable coagulation at the lowest overall treatment burden.
Jar testing is most useful when it reproduces the real process
A jar test is a decision tool, not a laboratory ritual. Its value depends on whether the test reflects actual plant conditions. Using untreated raw water, realistic coagulant concentrations, representative mixing intensity, and a meaningful settling period produces much more useful results than testing a broad chemical range under arbitrary conditions.
For routine optimization, compare a baseline dose with several narrow dose adjustments rather than testing only extreme concentrations. Observe more than final turbidity. Record pH after dosing, floc formation time, floc size, settling rate, supernatant clarity, and the volume or compactness of settled solids. A dose that produces slightly lower supernatant turbidity but substantially more loose sludge may not be the best operational choice.
Where polymers are used as coagulant aids, test them after selecting the primary coagulant range. Polymer dosage is highly sensitive: too little may not strengthen floc, while too much can create gelatinous solids, poor settling, filter blinding, or a slippery sludge that is difficult to dewater. The polymer make-down concentration, aging time, and feed-point location should be controlled as carefully as the nominal dose.
Jar-test results should be checked against plant performance rather than treated as final instructions. Differences in hydraulic detention, basin geometry, temperature, and mixing energy can change the full-scale response. A sensible practice is to use the test to identify a small operating range, then make controlled plant adjustments while watching settled-water turbidity, sludge blanket behavior, and filtration response.
Sludge reduction begins with avoiding unnecessary solids formation
Coagulation sludge contains both removed contaminants and chemicals introduced during treatment. The suspended solids in the raw water cannot be eliminated from the sludge balance, but avoidable chemical solids can. Excess aluminum or iron coagulant hydrolyzes into additional hydroxide solids, increasing sludge mass and often increasing its water content.
Reducing sludge does not mean underdosing coagulant. Underdosing transfers solids to downstream filters, shortens filter runs, and may create more difficult backwash waste. It means identifying the minimum dose that provides stable solids removal and then ensuring that mixing, pH, and polymer use are supporting that dose.
Sludge quality matters as much as sludge quantity. Dense, well-settling floc normally produces a more manageable underflow than weak, fluffy floc. If dewatering performance deteriorates after a chemical adjustment, assess whether the coagulant dose was raised unnecessarily, whether the polymer program changed, or whether the source water has introduced a different solids composition. Sludge blanket level, underflow solids concentration, and dewatering cake condition can reveal problems before disposal costs become obvious.
Use process signals to distinguish underdose, overdose, and poor flocculation
Several operational symptoms can look similar at first glance. High settled-water turbidity does not automatically mean insufficient coagulant. The pattern of observations is more useful than any single reading.
This distinction prevents the common cycle of increasing chemical feed whenever clarification deteriorates. Dose changes should be made deliberately, with enough time for the treatment train to respond. Frequent large corrections can destabilize a clarifier and make it difficult to identify the true cause of poor performance.
Chemical quality and storage discipline affect dose stability
Water Treatment Coagulants should be managed as process-critical chemicals. Differences in active content, basicity, impurity profile, density, or product age can change the actual amount of active material delivered by a fixed pump setting. Dose should therefore be expressed and tracked in a way that reflects active chemical basis where possible, not only pump speed or liters per hour.
Incoming batches should be checked against the agreed specification, and operating records should connect product batch, concentration, dose, raw-water condition, and treatment outcome. This is especially important when a new supplier, grade, or delivery route is introduced. A lower-priced product can increase overall cost if its concentration varies, its storage stability is poor, or its impurities complicate sludge handling and compliance monitoring.
Storage tanks, transfer lines, calibration columns, and metering pumps require routine verification. Sediment accumulation, crystallization, air ingress, degraded tubing, inaccurate flow meters, and uncalibrated pumps can all appear as “chemical performance” problems. The actual delivered dose should be checked periodically against the intended dose.
Not every industrial chemical associated with a water-related process is suitable as a coagulant. For example, Strontium Carbonate CAS#1633-05-2 is used in applications including ceramics, electronics, pyrotechnics, and sugar refining, but it is not a substitute for an approved coagulation chemical in potable-water treatment. Chemical selection must be based on intended use, water quality, local regulatory requirements, safety documentation, and compatibility with the treatment process.
A stable operating range is more valuable than a single “perfect” dose
The most practical endpoint is a documented operating window: a defined dose range linked to raw-water conditions, pH or alkalinity limits, mixing settings, polymer conditions where applicable, and expected settled-water performance. This gives operators a basis for controlled adjustment when source conditions shift.
A useful log does not need to be complicated. It should make it possible to see whether a turbidity event was accompanied by a pH change, a temperature change, a new raw-water source, a filter response, or a sludge-handling problem. Over time, this record turns dosing from a reactive pump adjustment into a process decision supported by evidence.
Lower turbidity and reduced sludge are compatible objectives when the treatment system is operated within its chemical and hydraulic limits. The effective approach is not to chase a single dose number, but to control the conditions that allow the selected coagulant to work efficiently: representative testing, correct mixing, stable pH and alkalinity, measured polymer use, verified feed accuracy, and close attention to downstream solids behavior.
Send Us Your Inquiry Today
