









Product Quick Navigation
Get a Quote
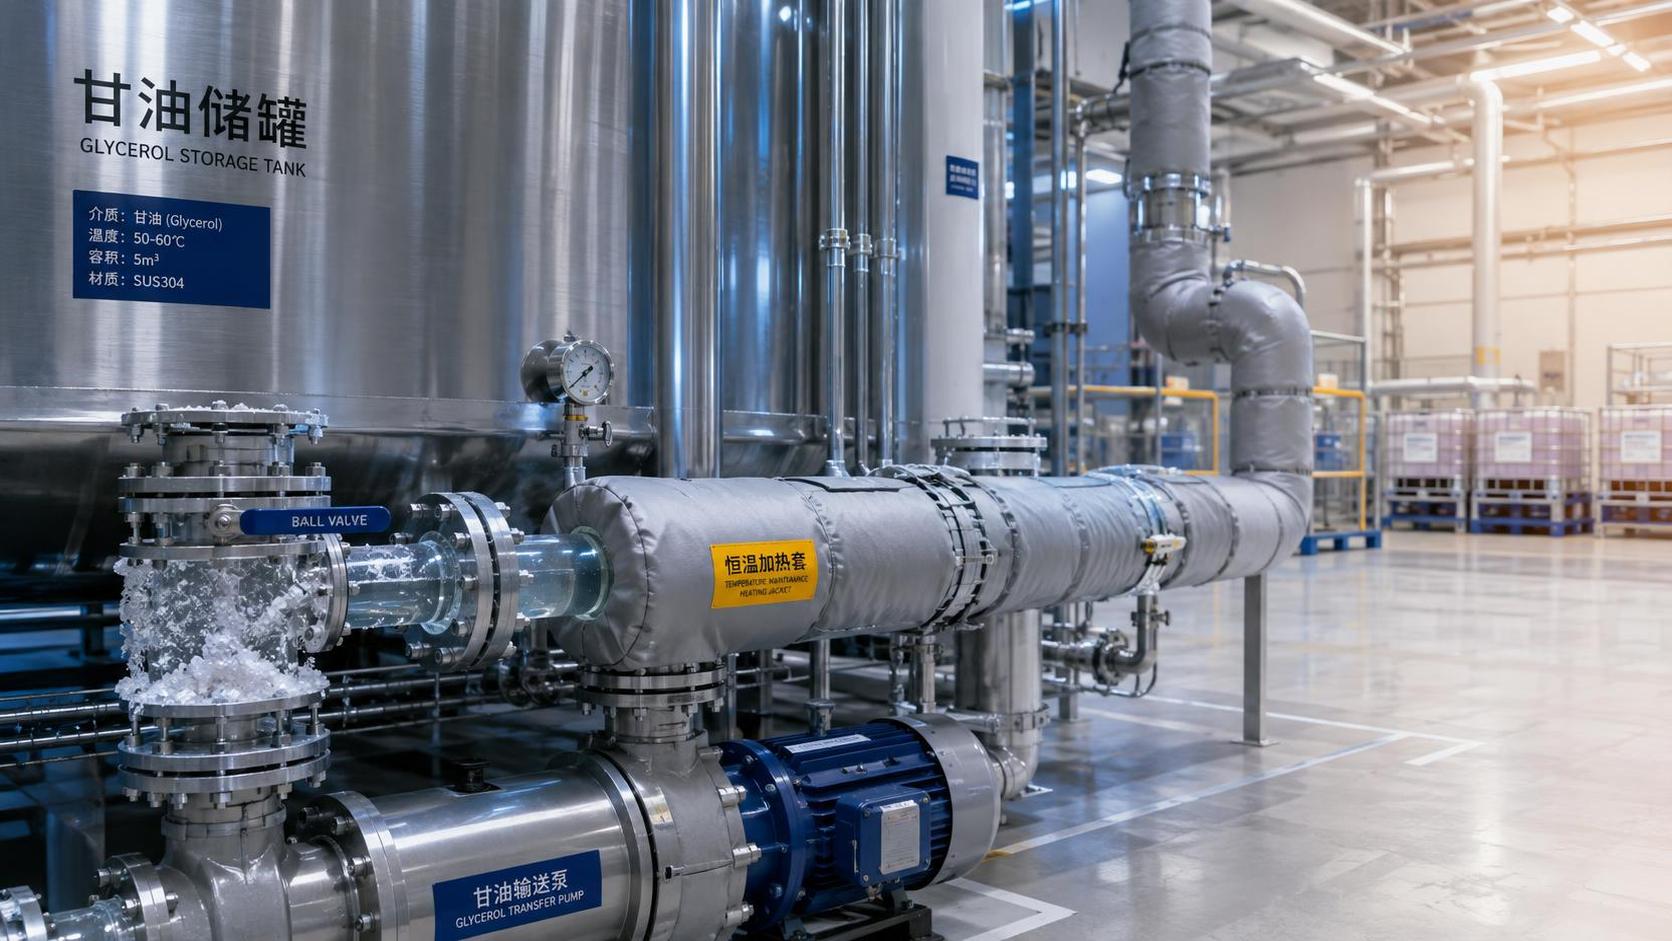
Glycerol can crystallize in storage even when the material was clear and easy to pump when received. The immediate operational symptoms are familiar: slow unloading, unstable pump suction, blocked strainers, high transfer pressure, or a drum that appears partly solid. In most cases, the issue is not product degradation. It is a physical phase change caused by storage conditions, composition, or local temperature differences within the container.
The practical response is to confirm whether the material has actually crystallized, restore it with controlled warming, and correct the storage condition that caused it. For maintenance teams, the most important point is that a clear top layer does not prove the entire container is liquid. Crystals often form first at cold walls, bottom outlets, valves, and low-flow sections of pipework, where they can disrupt transfer before the bulk product looks unusual.
Why glycerol crystallizes during storage
Pure glycerol has a relatively high freezing point compared with many liquid chemicals. Commercial glycerol may remain fluid at lower temperatures because water and other permitted components change its freezing behavior. That does not mean it is immune to crystallization. When temperature falls far enough, or when the composition is close to a crystallization-prone range, solid glycerol crystals can form.
Crystallization is often gradual. A container may be exposed to cold weather during transport, then moved into a warehouse where the outer wall warms but the center and lower portions remain cold. The material can therefore become non-uniform: liquid glycerol at the top, thickened product in the middle, and crystals near the discharge point. Attempting to pump from the bottom at that stage can overload equipment or create a misleading impression that the line has failed.
Four conditions usually deserve attention.
Do not confuse crystallization with contamination or a pump problem
Glycerol crystals are usually colorless or white and may look like a clear solid mass, granular deposit, or cloudy, thickened zone. The material may become more fluid as it warms. This behavior helps distinguish ordinary crystallization from some other problems, but it should not replace routine quality checks when the product’s history is unclear.
A blocked filter or pump can have several causes. Crystallization is likely when the issue follows cold storage, occurs at exposed piping or bottom outlets, and improves after uniform warming. It is less likely to be the only explanation when the material has unusual color, persistent foreign particles, a changed odor, or a known risk of cross-contamination. In those cases, warming the product may restore flow without resolving a quality issue.
Maintenance personnel should also avoid judging the product from a single surface sample. The warmest portion of a tote or tank may look normal while a cold layer remains at the outlet. Check the temperature at more than one accessible location and inspect the discharge valve, hose connection, pump inlet, and any low points in the transfer route.
How to restore crystallized glycerol safely
The aim is to warm the product evenly enough for the crystals to melt, then return the liquid to a uniform condition before transfer or use. Rapid, localized heating is a common source of repeat problems because it liquefies only the material closest to the heat source and can leave solid sections elsewhere.
- Stop forcing the transfer. Do not continue running a pump against a blocked line or increase pressure simply to overcome resistance. Thickened glycerol can place unnecessary load on seals, couplings, motors, and hoses.
- Check the container and line condition. Identify whether the restriction is in the bulk container, outlet valve, hose, filter, pump suction, or downstream piping. A cold valve may be the limiting point even after the drum body has warmed.
- Use gentle, controlled warming. A temperature-controlled warm room, suitable heating jacket, or compatible indirect heating arrangement is generally more reliable than applying intense heat to one spot. The heating method must be appropriate for the packaging and equipment in use.
- Allow time for heat to reach the center. Large containers warm slowly. Treating only the outside surface can create a liquid shell around a cold core. Keep the outlet closed until the material near the discharge area has returned to a workable condition.
- Mix only when the system is designed for it. If the container or storage tank has an appropriate agitation method, gentle mixing after partial melting can help equalize temperature and composition. Do not improvise agitation in a sealed package or introduce tools that could contaminate the product.
- Inspect before restarting normal use. Once flow is restored, check that no visible crystals remain around valves, filters, line bends, or pump inlets. A short controlled recirculation may be useful in a suitable closed system to confirm consistent flow.
Direct flame heating, uncontrolled steam contact, and aggressive spot heating should be avoided. These methods can damage packaging, create excessive local temperatures, and produce misleading results: the outer layer melts while the core remains solid. They also make it harder to identify whether the problem was cold exposure alone or a more complex handling issue.
Storage practices that prevent repeat crystallization
Prevention begins with the actual temperature profile, not the warehouse thermostat setting. A storage area may appear warm enough during the day while the loading bay wall, floor-level pallet position, exterior tank surface, or uninsulated transfer pipe falls much colder overnight. These local conditions often explain why only certain packages or lines are affected.
Keep glycerol in a stable indoor environment and protect it from prolonged cold exposure during receiving, staging, and transfer. For bulk storage, insulation and controlled heat tracing may be appropriate where seasonal temperatures or outdoor installation make cold spots likely. The design should cover vulnerable components, including outlet nozzles, valve bodies, pump suction lines, filters, and dead legs. Heating only the tank body does not protect a cold restriction downstream.
Storage instructions should be matched to the grade being handled. A higher-concentration glycerol grade and a water-containing grade should not automatically be managed using the same winter handling routine. Review the supplier’s product documentation for the delivered grade, including handling and storage guidance, before setting a fixed temperature policy.
Moisture control also matters, although it is often misunderstood. Glycerol is hygroscopic and can absorb water from air. An open vent, loose closure, repeated opening of drums, or unsuitable transfer practice can gradually change concentration. Water absorption may lower the tendency to crystallize, but it can make the product unsuitable for the intended process. Preventing crystals by allowing uncontrolled water pickup is not a valid solution.
Build the check into receiving and cold-weather maintenance
A useful after-sales procedure is to record the product grade, package type, arrival condition, estimated transit exposure, and storage location before a complaint develops. When a flow problem occurs, these details are more useful than a general statement that “the glycerol became solid.” They help separate a cold-chain issue from an equipment issue or a potential product-quality concern.
During cold periods, inspect vulnerable inventory before an urgent transfer is required. Prioritize packages stored near doors, exterior walls, unheated loading zones, or concrete floors. For tanks, include the lowest outlet and first sections of suction piping in routine checks. A small amount of crystallization at a valve can stop an otherwise serviceable tank from unloading.
It is also sensible to avoid moving cold glycerol directly into a process that depends on accurate dosing. Even if the product can be pumped, viscosity and temperature may still be uneven. Bring the material to a stable, homogeneous condition first, then resume normal metering. This reduces the risk of variable feed rates and avoids treating a storage problem as a process-control problem.
When supplier communication is needed
If crystallization recurs despite stable storage, gather practical evidence before escalating: the glycerol grade, batch identification, packaging condition, measured temperatures at several locations, length of cold exposure, photographs of the affected area, and the point at which flow stopped. This information allows the supplier to assess the situation against the grade’s handling requirements and determine whether sampling or further investigation is appropriate.
For international chemical supply, clear product documentation and responsive handling support are especially useful when materials move through different climates and storage systems. Huafeng Chemical supports overseas chemical trade with a broad product portfolio and foreign-trade service capability. For glycerol shipments, aligning package selection, expected transit conditions, receiving arrangements, and storage practices before delivery helps reduce avoidable cold-weather disruptions.
Questions that often arise during troubleshooting
Can crystallized glycerol be used after it melts?
If the issue is ordinary crystallization from cold exposure and the product has remained protected from contamination, it may return to a usable liquid state after controlled warming and homogenization. The decision should still follow the requirements of the intended application and the product documentation, particularly where concentration or purity is critical.
Will simply warming the pump solve the problem?
Not always. Warming the pump can help if the restriction is at the pump inlet or inside the pump. If crystals remain in the drum outlet, hose, filter, or upstream line, the pump may still starve or run under excessive load. Trace the full flow path before restarting.
Should water be added to make glycerol flow more easily?
Adding water changes the product composition and can affect downstream performance, specifications, and customer acceptance. It should not be used as an on-site remedy unless the process explicitly permits that adjustment and the resulting composition is controlled.
When glycerol becomes difficult to handle in storage, start with temperature distribution, product grade, and the exact location of the restriction. Controlled warming and a stable storage plan usually solve cold-induced crystallization. Repeated problems deserve a closer review of the complete path from transport exposure to the final transfer point, because the cause is often a cold valve, pipe section, or handling step that is easy to overlook.
Send Us Your Inquiry Today
