







Product Quick Navigation
Get a Quote
Alternatives to Thermoplastic Elastomers: Comparing Flexible Materials
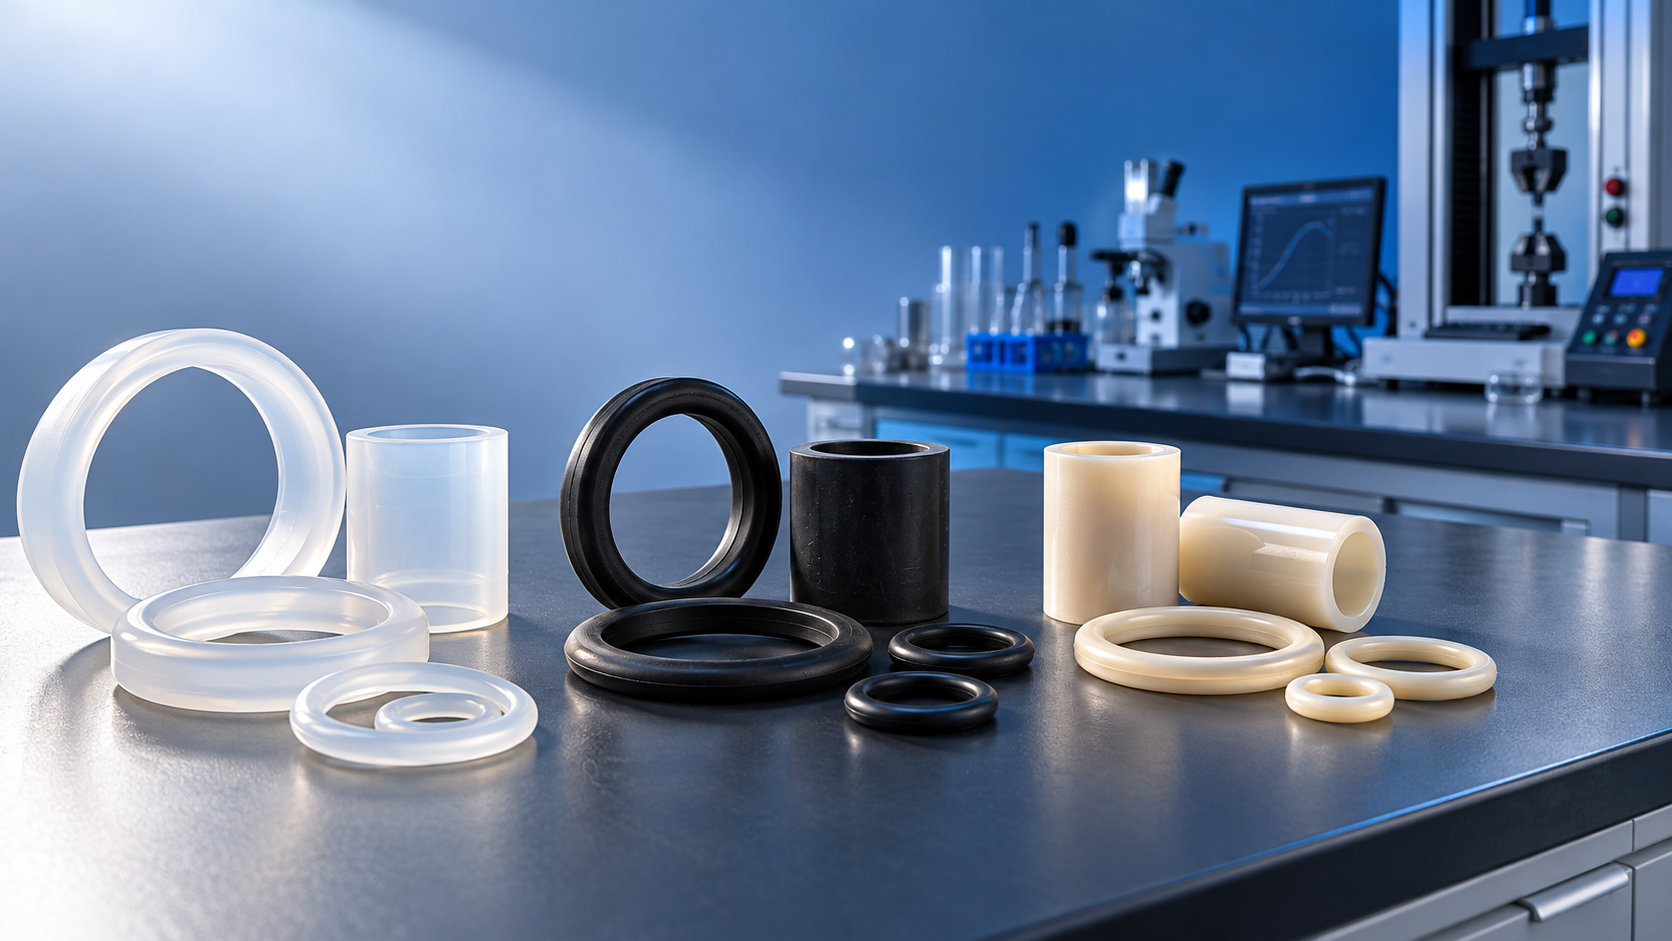
Choosing the right flexible material involves more than matching hardness or elasticity. Thermoplastic elastomer alternatives such as silicone rubber, polyurethane, natural rubber, and flexible PVC offer different trade-offs in temperature resistance, chemical compatibility, processing, cost, and regulatory suitability. The right choice depends on what the part must withstand, how it will be manufactured, and which compromises the application can tolerate.
A useful starting point is to define what “TPE” means in the existing design. Thermoplastic elastomers are a family, not a single material: styrenic TPEs, thermoplastic vulcanizates, and thermoplastic polyurethanes can behave quite differently. Replacing a soft-touch styrenic compound is a different exercise from replacing a TPV seal exposed to heat and automotive fluids. Without the current grade and its failure mode, a material comparison can quickly become misleading.
Start With the Failure, Not the Hardness
A matching Shore A hardness is useful for narrowing a shortlist, but it does not establish equivalence. Two compounds can feel similarly soft while differing substantially in compression set, tear resistance, friction, or stiffness at low temperature. Even hardness measurements can be distorted by specimen thickness, surface condition, and the measurement method.
Consider a gasket that seals correctly when new but leaks after months under compression. The issue may be permanent deformation, stress relaxation, chemical swelling, or a change in the mating surface—not insufficient initial softness. A replacement should therefore be assessed under the actual compression, temperature, and exposure conditions. For a grip or overmold, by contrast, surface feel, bond strength, abrasion, and resistance to skin-contact products may matter more than long-term compression set.
Before requesting samples, document the operating temperature profile, contact media, expected deformation, cleaning agents, service life, and relevant manufacturing process. Include occasional conditions such as a hot cleaning cycle or contact with an assembly lubricant. Those short exposures can determine the material choice.
Silicone Rubber: Strong Temperature Performance, With Design Caveats
Silicone rubber is often worth investigating for seals, tubing, and flexible components exposed to elevated temperatures or cold environments. Many grades retain flexibility across a broad temperature range and resist weathering well. That makes silicone a plausible candidate where a TPE hardens in the cold or loses sealing performance during heat exposure.
Its limitations are just as important. Silicone can be vulnerable to tearing, especially where a thin section contains a notch or is repeatedly stretched. It may also swell in some oils, fuels, and solvents; compatibility depends on the fluid and formulation. A seal that looks promising in dry heat testing should not be approved before immersion and post-exposure sealing tests.
Processing changes the calculation. Liquid silicone rubber and other cured silicone systems require curing equipment and tooling strategies that differ from those used for thermoplastic injection molding. Scrap cannot simply be remelted like an unvulcanized thermoplastic. For an overmold, adhesion to the substrate must be demonstrated with the selected grade, surface preparation, and process—not assumed from material family alone.
Polyurethane: Separate Thermoplastic and Cured Options
Polyurethane is a broad chemistry. Thermoplastic polyurethane, or TPU, is itself a TPE; it may be an alternative to a different TPE grade, but not an alternative to the TPE family as a whole. Cast or otherwise crosslinked polyurethane elastomers are a separate option when the design or production volume supports curing.
Polyurethanes are commonly considered for wheels, rollers, flexible bushings, and parts exposed to sliding wear. Their appeal is the potential combination of abrasion resistance, load-bearing ability, and elasticity. The formulation matters: a grade optimized for abrasion may not be the best choice for prolonged hot-water exposure or low-temperature flexibility.
Water and humidity deserve particular attention. Some polyurethane chemistries are more susceptible to hydrolytic degradation than others, so ask whether the proposed grade is intended for the expected moisture and temperature conditions. Also check processing requirements: moisture-sensitive thermoplastic grades may need controlled drying, while cast systems introduce mixing, curing, and dimensional-control considerations.
For a wheel, compare more than a material’s abrasion data sheet. Measure wear against the actual floor or track, under the expected load, with relevant contaminants present. A material that performs well against one abrasive surface may behave differently against another.
Natural Rubber and Other Cured Elastomers
Natural rubber is a credible choice where resilience, fatigue performance, or dynamic flexing drives the design. Mounts, vibration-control components, and repeatedly flexed parts are typical applications to consider. A well-designed natural rubber compound can offer a different balance of rebound and fatigue behavior from a soft thermoplastic compound.
The trade-off is environmental exposure. Natural rubber generally needs careful consideration where ozone, weathering, petroleum oils, or fuels are involved. Protective formulation and part design can help with some exposures, but they do not eliminate the need for testing. If oil resistance is central, a different cured elastomer such as nitrile rubber may be more appropriate; for outdoor weathering, EPDM may be worth screening. Neither should be treated as universally compatible with every fluid or service temperature.
Cured rubber also changes the production model. Vulcanization introduces cure time and process controls, and cured production scrap is not remelted into equivalent new material. On the other hand, a conversion may be justified if longer service life or lower failure risk outweighs the additional manufacturing complexity. Compare the finished-part economics, including rejects, assembly, and qualification—not just the price per kilogram.
Flexible PVC: A Practical Option When Formulation Is Controlled
Flexible PVC remains a candidate for applications such as tubing, profiles, cable coverings, and protective sleeves. It can be processed by established thermoplastic methods and formulated across a range of flexibility levels. For a straightforward extruded profile, the equipment and production route may be easier to adapt than a switch to a cured elastomer.
The point to investigate is the formulation, particularly its plasticizer system. Extraction, migration, or loss of plasticizer can change flexibility and create surface or compatibility problems over time. Contact with oils, solvents, adhesives, or other plastics deserves attention, as does low-temperature performance if the part must bend in cold conditions.
For food-contact, medical, electrical, or other regulated uses, request documentation for the specific compound and intended market. A statement that a resin is suitable for a broad application does not establish that every additive, colorant, and finished article meets the applicable requirements.
Formulation Can Change the Comparison
Material selection does not stop at the polymer name. Fillers, pigments, stabilizers, processing aids, and cure systems influence appearance and can also affect processing, mechanical behavior, and aging. When a candidate has been tested in black, for example, do not assume the white production compound will give identical results without verification.
White pigments are relevant to flexible plastics and rubber where opacity or consistent color is required. Titanium dioxide CAS#13463-67-7 is available in rutile and anatase forms and in different particle-size grades. Grade selection should account for dispersion, surface treatment, processing conditions, and the finished part’s requirements. The listed purity of at least 99.5% should be confirmed against the specification for the grade offered; it is not, by itself, evidence of suitability for a regulated application.
If outdoor appearance is important, evaluate the complete formulation after weathering rather than assuming that a white pigment guarantees UV durability. Likewise, ask for documentation specific to the supplied grade and destination market before relying on any compliance claim.
Build a Test Plan Around the Actual Part
Data sheets are useful screening tools, but comparisons are only meaningful when test methods and conditions are comparable. Tensile strength measured on a standard specimen does not predict how a thin molded corner will tear; compression-set results at one temperature and duration do not establish sealing performance at another.
A practical qualification sequence is to screen materials, make representative specimens or parts, expose them to service conditions, and then measure the property that matters. For a seal, that may mean leak performance after compression and fluid exposure. For a grip, it may mean bond strength after sweat, cleaning chemicals, and repeated handling. For tubing, it may include dimensional change, flexibility, and pressure-related performance after contact with the actual fluid.
Test the interactions as well as the material. A replacement can pass a fluid immersion test and still fail because it sticks to a mating surface, reacts with an adhesive, or shrinks differently in the tool. Where a part is overmolded, include substrate preparation and realistic production settings in the trial. A laboratory plaque is not a substitute for a molded assembly.
Use recognized methods such as ASTM or ISO procedures where appropriate, but specify the exact method, specimen, temperature, duration, and acceptance criteria in the purchase or qualification documents. The relevant standard and pass limits should be chosen for the application; a generic certificate cannot make that decision.
Supply and Documentation Are Part of the Selection
A material that passes the first trial can still create problems if the approved formulation changes or supporting documents are incomplete. Ask suppliers to identify the grade, manufacturing site where relevant, available technical data, batch traceability, and change-notification process. Confirm lead times and whether a second source would require its own qualification.
For cross-border chemical sourcing, Shandong Huafeng Chemical Co., Ltd. provides export services and a portfolio of chemical products from Shandong, China. When discussing a material or additive, the useful conversation is specific: required grade, destination, application, documentation, packaging, and delivery constraints. Regulatory status should be checked for the substance and supplied grade in the intended market, rather than inferred from a general product description.
The best replacement is the one that survives the relevant conditions and can be produced consistently. Keep the incumbent TPE as a control during testing, compare finished parts rather than family names, and resolve any documentation gaps before committing to tooling or a production change.
Send Us Your Inquiry Today
