







Product Quick Navigation
Get a Quote
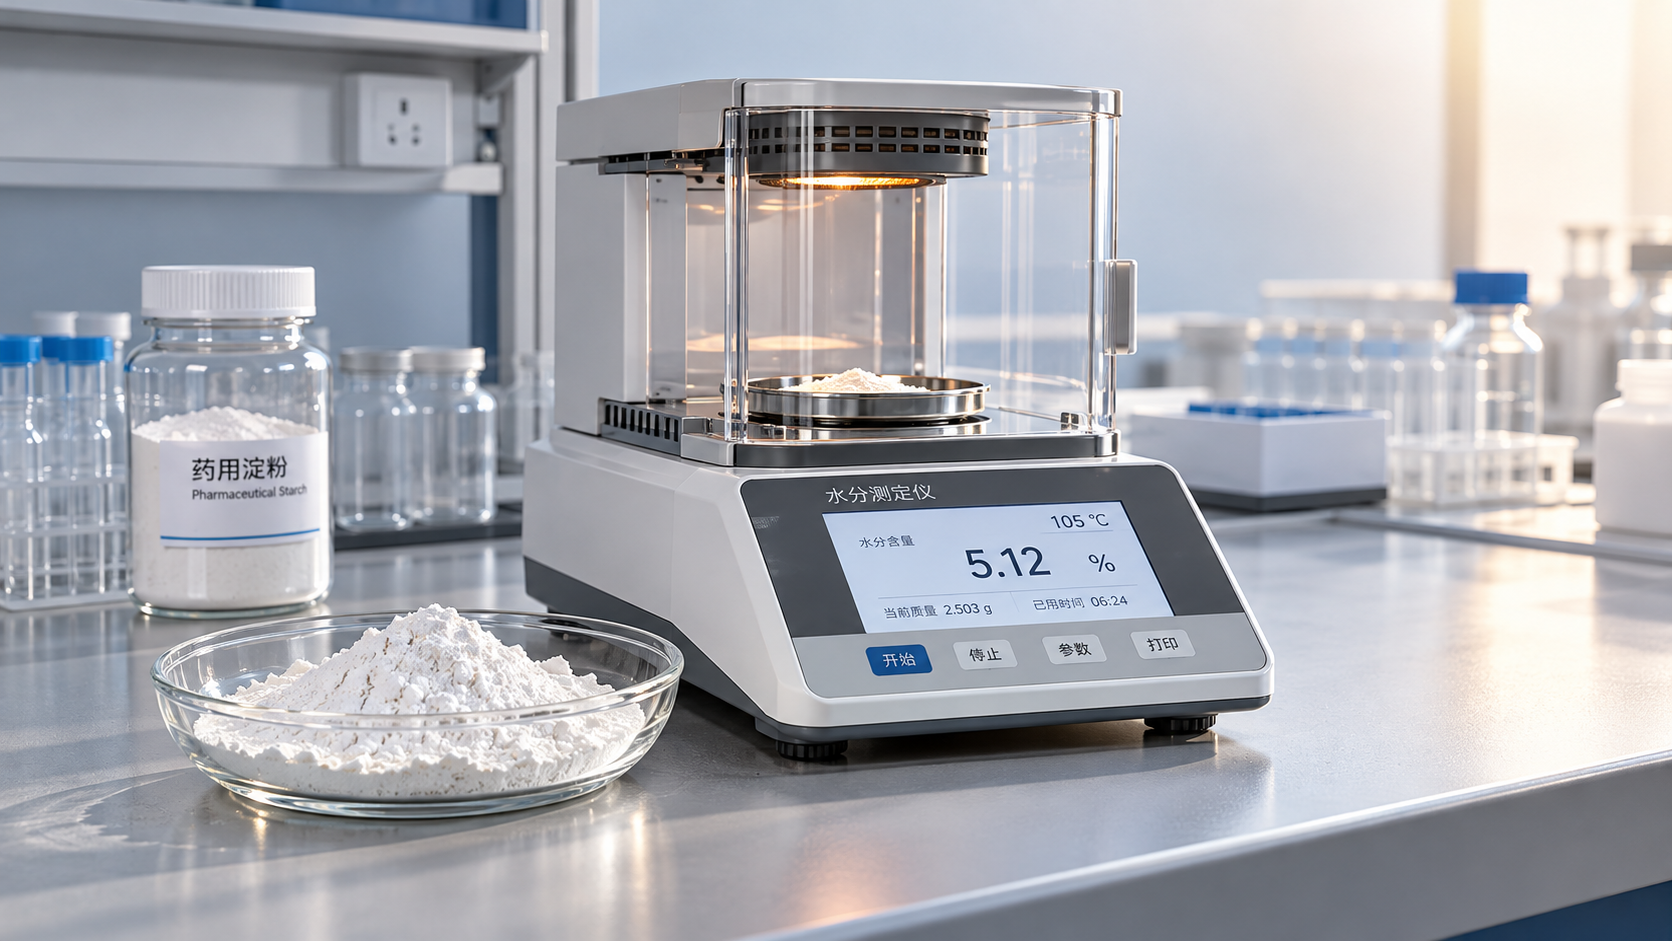
Moisture is a critical quality attribute when evaluating pharmaceutical starch, influencing its handling, storage stability, and compatibility with moisture-sensitive formulations.
Even small variations can affect powder flow, compaction, or product performance, depending on the application. The direction and magnitude of these effects require formulation-specific testing.
For technical evaluators, selecting low moisture pharmaceutical starch involves more than checking a single specification: it requires understanding the test method, acceptable limits, and supply consistency.
The practical objective is not necessarily the lowest possible moisture content. It is a justified, reproducible range that supports processing, stability, and the intended dosage form.
What Moisture Limit Is Appropriate for Pharmaceutical Starch?
There is no universal moisture limit that makes every starch suitable for every formulation. Acceptability depends on the material grade, analytical method, manufacturing process, and product requirements.
Start with the applicable pharmacopeial monograph and the manufacturer’s approved specification. Confirm the exact starch identity and grade before comparing any numerical limits.
Native starches and modified starches can have different properties and specification requirements. A value suitable for one material should not automatically become an acceptance criterion for another.
For a moisture-sensitive product, the compendial limit may not provide sufficient protection. A tighter supplier specification can be justified when formulation development or stability data support it.
Conversely, requiring an exceptionally dry material without evidence can restrict sourcing, increase cost, and create handling challenges. Establish a limit through risk assessment and representative batch studies.
Record whether the proposed limit applies at manufacture, release, delivery, or throughout the retest period. Those points are not interchangeable for a material that exchanges moisture with air.
Why Can Moisture Change Formulation Performance?
Starch contains water associated with its structure and can gain or lose moisture as environmental conditions change. Its measured content reflects both material characteristics and recent exposure.
In moisture-sensitive formulations, starch can contribute to the total water burden. The relevant question is whether that water becomes available to the active ingredient or other excipients.
Moisture transfer depends on formulation composition, temperature, relative humidity, and the moisture-sorption behavior of individual ingredients. Total water content alone does not predict the outcome.
For example, an active ingredient susceptible to hydrolysis may remain stable with one starch grade but degrade with another under the same manufacturing conditions. Confirm compatibility experimentally.
Moisture may also influence powder flow, adhesion, and agglomeration. A batch that performs acceptably in a laboratory can behave differently after exposure to humid production air.
During compaction, changes in moisture can affect particle deformation and bonding. Depending on the formulation, that may alter tablet hardness, friability, disintegration, or dissolution.
Very low moisture is not automatically beneficial. Excessive drying or extended exposure to dry air can change handling or compaction behavior, so assess the complete operating range.
For granulation processes, the initial moisture of each ingredient can affect the amount of liquid needed and the final drying endpoint. Account for incoming variability during development.
These effects are formulation-specific rather than guaranteed outcomes. Link each proposed moisture limit to a measurable product or process attribute instead of relying on general assumptions.
How Should Moisture Be Measured and Compared?
Before comparing supplier results, identify exactly what each test measures. Loss on drying and water-specific methods answer related but different questions.
Loss on drying measures the mass lost under defined conditions. Depending on the material and procedure, that loss can include volatile substances other than water.
Karl Fischer titration measures water through a chemical reaction. The sample preparation and extraction conditions must still be appropriate for the starch grade and its water distribution.
Results from the two methods should not be treated as interchangeable without evidence. A specification must name the method, operating conditions, and reporting basis used for acceptance.
For loss on drying, review the sample quantity, drying temperature, duration or endpoint, and equipment. Differences in these details can produce meaningfully different results.
For Karl Fischer analysis, assess sample handling, extraction efficiency, reagent suitability, and potential interference. Method suitability should cover the expected moisture range and sample matrix.
Use a representative sample and minimize exposure during sampling, weighing, and transfer. An open container in a humid laboratory can compromise an otherwise reliable measurement.
Confirm whether results are expressed on an as-received or dry basis. A numerical comparison is misleading when the basis, method, or conditioning history differs.
When changing methods or suppliers, analyze representative batches using both approaches. Establish an evidence-based relationship where possible, but do not assume a constant conversion factor.
Review method precision near the proposed specification limit. If analytical variability is large relative to the acceptance range, borderline batch decisions may be difficult to defend.
How Do You Set a Defensible Incoming Specification?
Begin by identifying the critical quality attributes that moisture could affect, such as degradation, blend uniformity, tablet strength, disintegration, or process yield.
Next, assess the proposed starch grade across a practical moisture range. Include material near both the lower and upper boundaries expected during supply and manufacturing.
Where feasible, manufacture representative blends or batches under controlled humidity. Measure the response of the process and the finished product rather than only the incoming excipient.
Use stability studies to examine whether initial starch moisture affects degradation, dissolution, or other relevant attributes over time. Include the intended packaging and storage conditions.
Set acceptance criteria using the combined evidence from development, analytical capability, supplier variability, and applicable standards. Document the rationale and any assumptions requiring later verification.
Consider whether a maximum alone is adequate. A lower boundary or operating range may be useful when very dry material produces inconsistent processing or performance.
Distinguish a supplier’s release specification from an internal alert limit. An alert can trigger investigation or enhanced monitoring without automatically making a conforming batch unacceptable.
When tightening an existing limit, check the effect on sourcing and investigate historical batch data. A specification should control a demonstrated risk and remain consistently achievable.
Which Supplier Documents and Batch Data Matter?
Request a current specification and a certificate of analysis for each delivery. The certificate should identify the batch, test results, method references, and applicable acceptance criteria.
Review actual results rather than only a statement of compliance. Several batches near the upper limit may present a different operational risk from consistently lower results.
Ask for representative historical data covering normal production variability, seasonal conditions, and relevant manufacturing sites. A small sample cannot establish long-term capability on its own.
Confirm the material’s botanical source, modification status, manufacturing site, and intended pharmaceutical grade. Also request applicable compendial compliance and excipient quality documentation.
Assess change-control arrangements for manufacturing location, raw materials, drying conditions, packaging, analytical methods, and retest periods. Changes may affect performance even when specifications remain unchanged.
Supplier qualification should also address traceability, quality agreements, deviation handling, and the availability of investigation records. Independent audit needs depend on the purchaser’s risk assessment.
For imported materials, verify who controls storage and transport after release. A compliant certificate does not by itself establish the condition of the material upon arrival.
Shandong Huafeng Chemical Co., Ltd. describes itself as a chemical export service provider. Technical buyers should confirm the actual starch manufacturer, grade, documentation, and supply arrangements directly.
How Should Packaging, Storage, and Transport Be Assessed?
A low initial moisture result is useful only if packaging and handling preserve an acceptable condition until use. Evaluate the complete route from manufacture to dispensing.
Request the packaging configuration, liner material, closure method, and recommended storage conditions. Check whether the proposed barrier is supported by stability or packaging-performance data.
Review shipment duration, expected temperature and humidity exposure, warehouse conditions, and the possibility of condensation. Seasonal routes may present different risks for the same product.
Inspect containers upon receipt for damage, compromised seals, or visible moisture. Define quarantine and investigation procedures before accepting material with evidence of packaging failure.
After opening, reseal containers promptly and control exposure during dispensing. Establish a justified in-use period when repeated opening could affect the material’s moisture content.
If repacking or extended storage is necessary, evaluate moisture changes under representative conditions. Retesting should use a suitable method and a sampling plan that reflects the risk.
Moisture is not the only storage concern. Microbiological quality, contamination prevention, and the manufacturer’s recommended retest period should also be considered for the selected grade.
How Can Compatibility and Moisture Transfer Be Tested?
Begin with a risk-based compatibility screen involving the active ingredient, starch, and other moisture-sensitive components. Include controls so observed changes can be attributed more confidently.
Condition representative materials at relevant humidity levels, then measure their moisture and evaluate chemical or physical changes. Select conditions that reflect both intended use and potential excursions.
Moisture sorption data can help explain how materials respond to relative humidity. They can also inform packaging and environmental controls, but they do not replace formulation testing.
Where appropriate, measure water activity as a complementary indicator of water availability. It is distinct from total moisture content and should not be substituted for a validated specification.
Compare blends containing starch at different moisture levels, then monitor active ingredient degradation, impurities, and relevant physical properties using stability-indicating methods.
Extend promising laboratory findings to representative manufacturing conditions. Mixing time, hold time, granulation liquid, drying, and compression can all influence the final outcome.
For a supplier change, compare more than the moisture certificate. Particle size, morphology, functionality, and other grade-specific properties may also explain performance differences.
Document the acceptance decision alongside the evidence. If the material is suitable only within a particular humidity range or hold time, make that restriction operationally visible.
How Should Other Powdered Ingredients Be Evaluated?
Do not assume that moisture-related claims for one ingredient apply to another. Each powder needs its own identity, grade, specification, and intended-use assessment.
For example, Adipic acid CAS#124-04-9 is a separate organic acid offered for applications including food and cosmetics, with buffering among its stated functions.
Its listed characteristics include a white solid appearance and a storage recommendation below 30°C. Confirm the relevant grade, current specification, and suitability before considering any application.
It is not pharmaceutical starch or a substitute for it. Any proposed use in a pharmaceutical formulation requires independent assessment of regulatory status, compatibility, and quality requirements.
What Should an Evaluation Decision Include?
A sound decision combines the incoming specification with evidence that the material performs as intended. No single moisture result can establish suitability for every product.
Confirm the exact starch grade and applicable standards; compare results only when methods and reporting bases align; and test the material across a justified moisture range.
Then verify supplier consistency, packaging protection, storage controls, and change notification. Define what happens when results approach limits or when transport conditions are uncertain.
Ultimately, low moisture pharmaceutical starch is valuable when its moisture range is controlled in a way that supports the specific formulation and process throughout its supply life.
Send Us Your Inquiry Today
