







Product Quick Navigation
Get a Quote
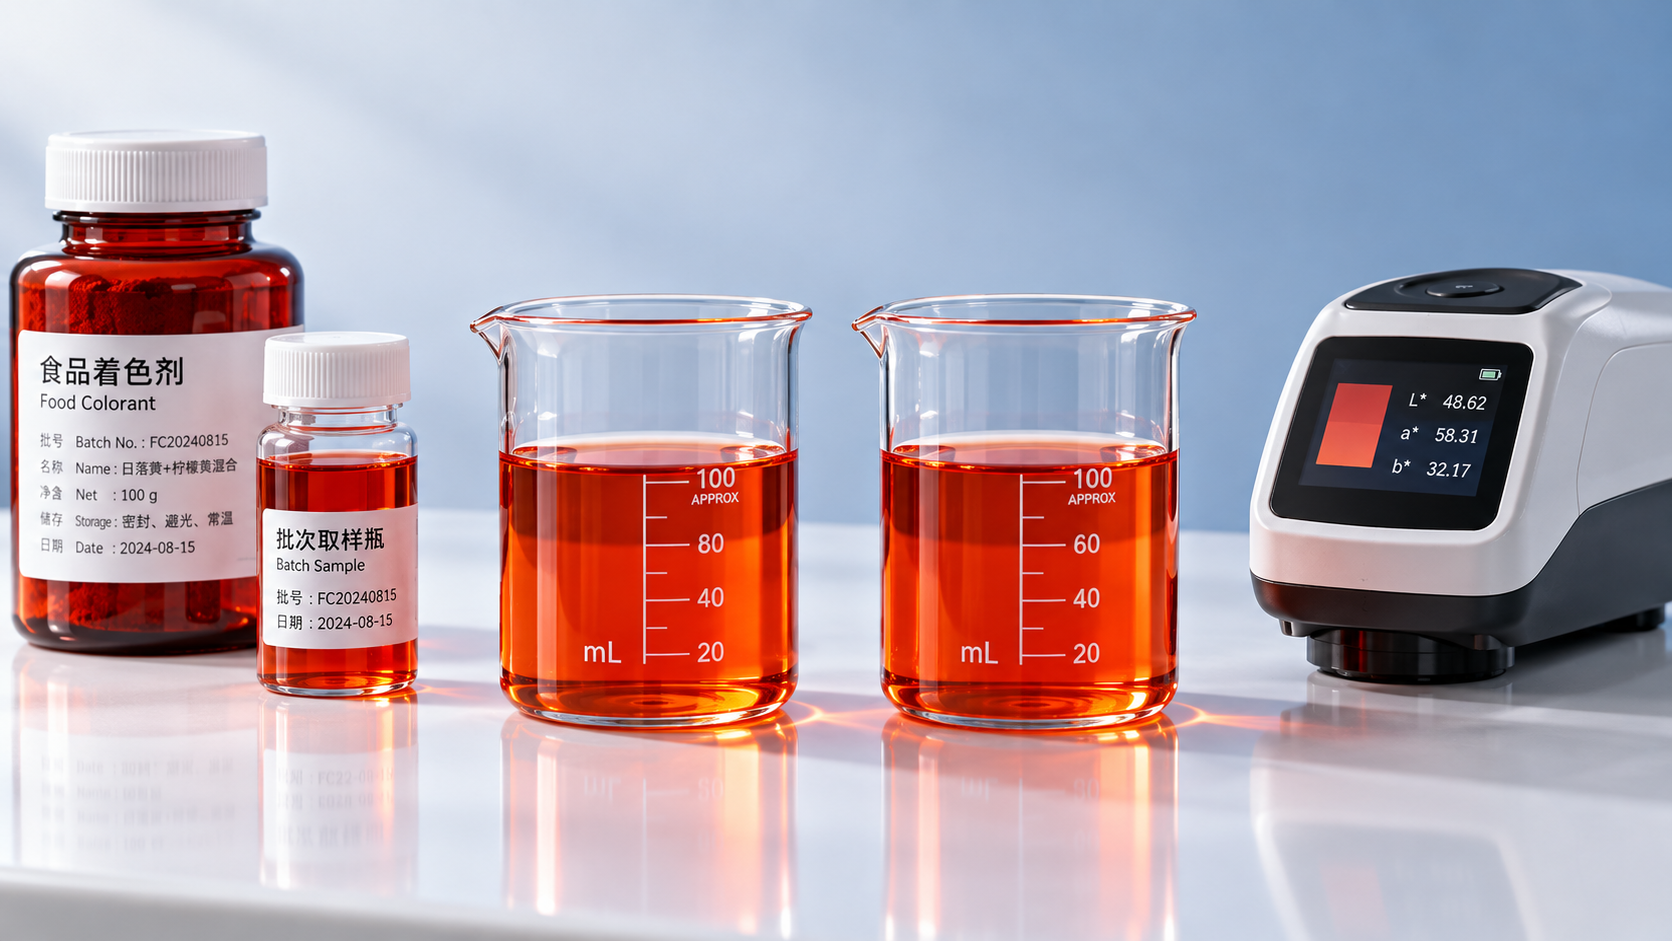
Small food colorant samples can represent production batches, but only when their source, collection method, and handling are controlled. A successful laboratory trial shows that the material tested can work in a particular formulation. It does not, by itself, establish that a future shipment will have the same color strength, shade, dispersibility, or processing stability.
The decisive question is not how small the sample is, but what it represents. A traceable sample taken from a finished commercial lot provides stronger evidence about that lot than an untraceable demonstration sample. Even then, approval should connect three separate findings: the lot meets its specification, the sample adequately represents the lot, and the material performs acceptably in the intended food application.
A development sample and a shipment sample answer different questions
A development sample is useful for deciding whether a colorant is technically suitable. It may establish the required dosage, identify interactions with acidity or heat, and help select between water-soluble dyes, insoluble lakes, or formulated natural colors. It may come from laboratory preparation, pilot production, or existing commercial inventory. Those origins are not interchangeable.
A sample from a finished production lot answers a narrower question: whether material from that identified lot meets the agreed requirements. Its value depends on how it was collected. A scoop from one accessible location cannot demonstrate uniformity across a blender, filling run, or shipment containing several lots.
A retained reference sample serves another purpose. It preserves evidence of an approved material for later comparison. Its label should identify the product, lot, sampling date, and storage conditions. If the reference deteriorates during storage, it can become a misleading benchmark rather than a reliable control.
Before approving a sample, obtain a clear statement of its origin. “Same product” is insufficient if the sample and shipment differ in manufacturing site, formulation revision, strength grade, carrier system, or physical form.
Why a matching product name does not guarantee matching performance
Batch variation can arise from the color-producing material itself or from how it is formulated and processed. For botanical extracts and other naturally derived colors, variation in source material and processing can affect pigment composition. Standardization can control color strength without making every secondary characteristic identical.
For blended products, the proportions and uniform distribution of components matter. A blend can meet an overall strength target while showing a different hue if the balance between pigments changes. Carriers, moisture, particle size, and dispersion behavior can also affect the result at the point of use.
Physical separation creates a different problem: the batch average may be acceptable while individual portions are not. Powder components with different particle sizes or densities can segregate during transfer and transport. Liquid dispersions can settle where the formulation permits it. A sample collected after controlled mixing may therefore differ from material withdrawn from an unmixed container.
These mechanisms require different responses. Adjusting the dosage may compensate for a strength difference, but it cannot reliably correct a changed hue, poor dispersion, or reduced heat stability. A visual mismatch should trigger investigation rather than an automatic increase or decrease in addition rate.
Make the sample traceable to the material being purchased
The purchase specification should define what constitutes a lot and whether a shipment may contain multiple lots. A single sample should not be treated as evidence for several independently manufactured batches merely because they share a product code.
For shipment approval, the sampling arrangement should address:
- Sampling point: whether material is collected from the finished bulk batch, the filling stream, or packed containers.
- Coverage: how increments cover relevant locations, containers, or stages of filling.
- Sample preparation: whether increments remain separate or are combined into a composite.
- Identification: the lot number, collection date, sampler, and relationship to the shipment.
- Preservation: packaging, sealing, and storage that protect the sample from moisture, light, contamination, and temperature damage.
There is no universally valid number of containers to sample. The plan should reflect lot size, product form, manufacturing controls, previous variability, and the consequence of failure. Where segregation is a credible concern, testing separate increments can reveal differences that a composite sample would average out.
Sample quantity still matters operationally. There must be enough material for analytical testing, application trials, repeat testing, and retention. However, a larger sample collected poorly is not necessarily more representative than a smaller sample collected under a sound plan.
Use the COA to verify a lot, not to assume application equivalence
A batch-specific certificate of analysis is an important link between the sample and the shipment. It should identify the manufacturer or responsible issuing entity, product, lot, specification, and relevant test results. Dates and shelf-life information should be consistent with the labeling and supporting records.
The useful question is not simply whether a COA exists, but whether its tests address the reasons the material might fail. Depending on the colorant, relevant characteristics can include identity, color strength, moisture, pH, insoluble matter, microbiological quality, and specified contaminants. Not every parameter applies to every product.
Food colorant COA batch consistency also depends on comparable methods. Strength values cannot be meaningfully compared without understanding the measurement basis, solvent or medium, dilution, wavelength where relevant, and whether results are reported on an as-is or other defined basis. Numerical agreement under different methods may be misleading.
A result reported only as “passes” can confirm compliance with a limit but provides little information about the direction or size of variation. For performance-critical attributes, request actual values where appropriate and compare several commercial lots tested by the same method. This helps distinguish a repeatable production range from one favorable sample; it does not prove future capability by itself.
A COA is also not evidence that every container is uniform unless the underlying sampling and control system supports that conclusion. Nor does compliance with a supplier’s specification necessarily mean that the material will satisfy a narrower finished-food color requirement.
Compare samples under conditions that expose meaningful differences
Looking at powders in their containers is a weak acceptance test. Apparent color changes with particle size, packing, moisture, lighting, and viewing angle. Two powders that look different can produce similar finished-food shades; two similar-looking powders can behave differently after dissolution or processing.
A useful comparison separates intrinsic color performance from application performance.
Under controlled laboratory conditions, compare the approved reference and candidate lot using the same preparation method, concentration basis, water quality, pH, temperature, and measurement timing. Where relevant, assess dissolution or dispersion time, sediment, and visible specks as well as color. Instrumental measurements should use consistent geometry and sample presentation.
In the food matrix, reproduce the variables that determine performance: acidity, heat exposure, addition sequence, mixing, fat content, packaging, and storage. An immediate match in a clear solution does not establish equivalent behavior in an opaque dairy product or an acidic beverage after processing.
Equal-dose and strength-normalized comparisons answer different questions. Equal-dose testing reveals what happens if the production recipe remains unchanged. Strength-normalized testing helps determine whether a difference is primarily concentration-related or persists after adjustment. Both can be useful, but the basis must be stated.
If instrumental color difference is used, agree on the calculation method, measurement conditions, and acceptance limit before testing. No single color-difference threshold is suitable for every food. Appearance also depends on gloss, opacity, surface texture, and package presentation, which a measurement alone may not fully capture.
Set acceptance rules before the shipment is released
“Match the approved sample” leaves too much open to interpretation. An operational specification should identify the reference, preparation method, relevant analytical limits, application test, and permitted variation. It should also distinguish mandatory safety or legal requirements from performance targets.
This distinction determines the response to a deviation. A modest strength difference within an agreed operating range may be manageable through a validated dosing adjustment. An identity failure, prohibited constituent, or contaminant result outside an applicable limit is not a shade-adjustment problem.
For an initial commercial order, approval can be conditional: laboratory suitability is accepted, but shipment release depends on evidence from the actual production lot. A representative pilot-scale application can provide additional confidence where laboratory processing does not reproduce commercial heat transfer, shear, or mixing.
Future supply requires more than one successful lot. Commercial-lot comparisons, retained samples, and change-notification agreements help control continuity. Relevant changes include manufacturing site, pigment source, carrier composition, standardization method, and production process. A product code should not silently remain unchanged while characteristics important to the approved application change.
Keep compliance evidence separate from color approval
A successful application trial does not establish that a colorant is legally suitable for the destination market or intended food category. Authorization, identity and purity requirements, use restrictions, and labeling obligations must be checked against the actual composition and proposed use. A trade name alone is not enough.
Alongside the batch COA and product specification, supporting information may include composition and carrier declarations, allergen information, traceability records, storage instructions, and applicable safety documentation. The required package depends on the product, destination, and contractual obligations. An SDS, where required or provided, addresses handling hazards; it does not replace food-use compliance evidence.
Where halal status is a purchasing requirement, a food colorant halal certificate should cover the relevant product and manufacturing scope and be acceptable for the intended market or certification arrangement. It does not establish batch shade consistency, color strength, or compliance with every destination’s food additive rules.
Documentation becomes useful when it links to the material actually supplied. Conflicting product names, unexplained manufacturing entities, or a certificate covering a different formulation should be resolved before release.
When the delivered material does not match
If imported food colorants fail incoming inspection, quarantine the affected stock and preserve the evidence before attempting correction. Record the lot, container condition, sampling location, preparation method, and test results. Repeat testing should follow an agreed procedure, not repeated adjustments until a passing result appears.
Compare the incoming sample with the approved reference and, where available, the supplier’s retained sample from the same lot. This can help distinguish production variation from sampling error, transport damage, storage deterioration, or differences between test methods. A satisfactory supplier retain does not automatically invalidate an incoming failure: the two samples may represent different portions or handling histories.
Opened samples need controlled storage as well. Follow the product-specific instructions, reseal promptly, and record opening dates and any preparation or reconstitution. If mixing is required before withdrawal, use the specified procedure rather than assuming that every liquid or dispersion should be handled identically.
Shade correction during production should proceed only within a validated formulation and applicable use limits. It is not a remedy for failed identity, safety, or compliance requirements. The strongest approval decision is therefore not “the small sample looked right,” but “the identified lot was sampled appropriately, met agreed requirements, and performed within defined application limits.”
Send Us Your Inquiry Today
