









Product Quick Navigation
Get a Quote
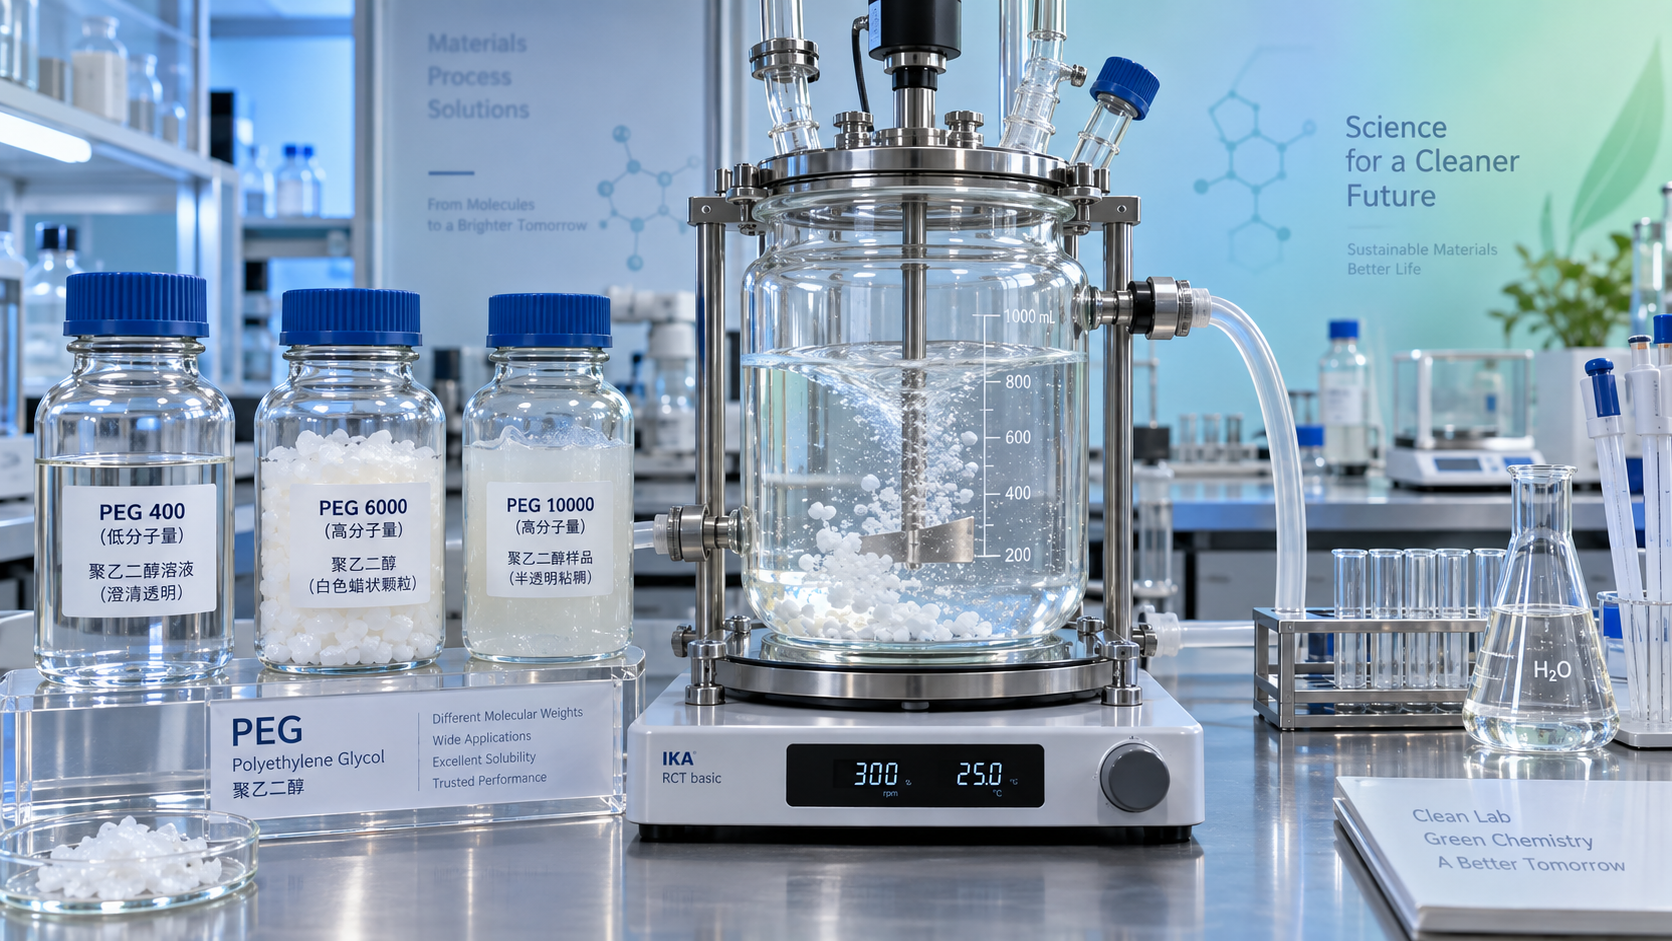
A formulation can fail its first processing trial even when the purchase order matches the requested material name. The usual cause is that “Polyethylene Glycol” describes a family, not a single functional material. A liquid PEG that dissolves quickly in water may be unsuitable where a waxy solid is needed for controlled melt behavior; a higher-molecular-weight grade may provide the desired body but dissolve too slowly or create unacceptable viscosity during mixing.
The practical starting point is direct: select PEG molecular weight according to the physical state, viscosity range, dissolution route, and performance required in the finished system. Molecular weight is the main selector because it governs whether the material behaves as a low-viscosity liquid, a soft paste, a wax-like solid, or a higher-melting polymeric carrier. Solubility must then be verified against the real solvent system, concentration, temperature, and order of addition rather than assumed from a general statement that PEG is water-soluble.
Begin with the job the PEG must perform
Before comparing grade numbers, define the material’s role. Polyethylene Glycol may act as a solvent, humectant, processing aid, dispersing medium, lubricant, binder, release aid, carrier, plasticizer, or viscosity modifier. One grade rarely performs all of these roles equally well.
For example, a technical evaluator reviewing a liquid formulation may need fast incorporation at ambient temperature and minimal thickening. In that case, a lower-molecular-weight liquid grade is usually the logical starting point. A tablet-coating, hot-melt, polishing, or solid-processing application may instead require a material that remains solid during storage, melts within a controlled operating window, and contributes structural consistency. The right selection depends on the function, not merely on whether the grade can technically dissolve.
It is useful to document the intended role in one sentence before requesting samples: “PEG is needed as a water-miscible carrier at room temperature,” or “PEG is needed as a solid binder that melts during processing but remains stable in finished goods.” This statement filters out many unsuitable grades early.
How molecular weight changes handling and performance
PEG grades are commonly identified by approximate average molecular weight. The number is not a guarantee of identical behavior across all suppliers, because grade specifications, molecular-weight distribution, hydroxyl value, moisture, and impurity limits may differ. It remains the most useful first indicator of physical form and expected processing behavior.
As molecular weight rises, PEG generally becomes more viscous and more solid at room temperature. Melting or softening behavior also becomes increasingly important. A grade selected only because it offers higher viscosity may create difficulties in pumping, filtration, deaeration, or complete dissolution. Conversely, replacing a solid PEG with a lower-molecular-weight liquid may make an initially smooth process easier while weakening the final product’s structure or changing release behavior.
Do not treat the grade number as an isolated parameter. A nominal PEG grade should be reviewed together with appearance, acid value where relevant, water content, hydroxyl value, color, ash or residue limits, and the supplier’s stated molecular-weight range. These details become especially important when PEG is used in sensitive formulations or repeated production campaigns.
Solubility is a system property, not a catalog label
Most PEG grades are readily soluble in water, but real-world dissolution can still be slow, incomplete, or operationally inconvenient. The issue is often not whether the polymer is soluble in principle. It is whether the chosen grade can dissolve at the required concentration, at the available temperature, within the allowed batch time, and without creating localized gel-like regions.
Higher-molecular-weight grades may need heating, stronger agitation, or a staged addition method. When flakes or powder are added rapidly into a limited volume of water, the outer surface can hydrate first and form a viscous layer that slows penetration of the remaining material. This can be mistaken for poor solubility. It is often a mixing and addition problem rather than an incompatibility problem.
Solubility in organic media requires more caution. PEG compatibility varies with the solvent’s polarity, water content, temperature, and the presence of salts, surfactants, acids, bases, or other polymers. A grade that forms a clear solution in one polar solvent blend may separate, haze, or remain partially swollen in another. If the finished formulation contains electrolytes, the effect on phase behavior should be checked at the intended use concentration rather than with a dilute bench sample.
Questions that should be answered during screening
- What is the target PEG concentration in the finished formulation?
- Will mixing occur at ambient temperature, under controlled heating, or in a melt process?
- Is the material added to water, solvent, a surfactant phase, or a multi-component blend?
- What clarity, homogeneity, and filtration requirements apply after dissolution?
- Does the process allow the time required for the selected grade to wet and dissolve fully?
- Will the formulation encounter cooling, freezing, concentration changes, or long storage that may alter phase behavior?
A small compatibility test should reproduce the intended sequence of addition. Adding PEG to water can behave differently from adding water to a PEG-rich phase. For solid grades, record temperature, agitation type, addition rate, dissolution time, and appearance after cooling. These observations are more useful for grade selection than a simple pass/fail statement made under uncontrolled laboratory conditions.
Use viscosity as a process limit, not just a product attribute
Viscosity is often the variable that turns an apparently acceptable PEG grade into a manufacturing problem. It affects pump selection, transfer speed, agitation load, heat transfer, dosing accuracy, and the ability to remove entrained air. A specification sheet may show viscosity at a stated temperature, yet the actual process can operate several degrees lower or higher. That difference can be significant, especially for intermediate and high molecular weight grades.
When evaluating a liquid or semi-solid grade, establish the lowest temperature likely during receiving, storage, and transfer. A material that flows well in a warm laboratory may be difficult to pump after warehouse cooling. For a solid grade, confirm whether melting is allowed and whether the available vessel can heat uniformly without local overheating. The material should also be evaluated after one or more heat-cool cycles if the process involves remelting.
Finished-product viscosity must be considered separately from neat PEG viscosity. In a water-based system, PEG may increase, decrease, or otherwise modify apparent viscosity depending on the co-formulants. It can plasticize certain polymer networks, alter micellar structures in surfactant systems, or change the hydration behavior of other thickeners. A grade chosen to “increase viscosity” should therefore be tested in the actual formulation, not judged only by its own viscosity value.
Match grade selection to common application patterns
Liquid carrier or moisture-retention applications: Lower molecular weight PEG grades are often considered where easy dispensing, rapid miscibility, and a liquid form are priorities. Screening should focus on odor, color, water content, stability with active ingredients, and the effect on final texture. Where the formulation contains volatile components, confirm whether PEG changes evaporation or phase balance during storage.
Aqueous processing and controlled viscosity applications: Intermediate grades can provide a useful balance between water compatibility and body. They may be appropriate where a completely low-viscosity liquid would run too freely but a solid grade would complicate handling. The main risk is underestimating temperature sensitivity. Test at both production temperature and the lowest expected storage temperature.
Solid dosage, coating, and melt-processing applications: Higher molecular weight PEG grades are commonly assessed for their wax-like character and melt behavior. Selection should include melting or softening range, particle form, flow during feeding, blend uniformity, and recrystallization behavior after cooling. In these applications, the grade can influence mechanical strength, surface feel, dissolution characteristics, or processing torque.
Industrial formulations: In lubricating, ceramic, textile, cleaning, and polymer-processing contexts, compatibility with the entire system may outweigh water solubility alone. Check interactions with salts, fillers, pigments, resins, and surfactants. Handling assumptions should not be transferred between unrelated raw materials: a low-water-solubility inorganic powder such as Magnesium fluoride CAS#7783-40-6 requires a very different dispersion and exposure-control review from a water-compatible PEG grade.
Where technical evaluations often go wrong
One frequent mistake is specifying only “PEG” with no grade, physical form, or critical quality limits. This leaves the supplier to interpret the requirement and may result in a material that is technically PEG but operationally unsuitable. The purchase specification should identify the desired grade or molecular-weight range, acceptable appearance, form, relevant purity limits, packaging expectations, and any application-specific documentation required by the internal quality system.
Another error is evaluating dissolution using a concentration far below production conditions. A grade may dissolve immediately at low concentration but become slow to incorporate near the actual formulation level. Similarly, testing only while warm can conceal clouding, crystallization, or viscosity increases that appear after cooling.
Substituting one PEG grade for another by weight alone is also risky. A lower molecular weight replacement may alter plasticization, wetting, migration, or moisture response. A higher molecular weight replacement may increase batch time, create incomplete dissolution, or change the solid-state properties of the finished material. Any substitution should be treated as a formulation change, even when the chemical family is the same.
A practical approval sequence
- Define the functional target. Identify whether the PEG must act primarily as a liquid carrier, solvent, binder, humectant, lubricant, processing aid, or solid matrix component.
- Set the physical operating window. Record storage temperature, transfer conditions, mixing temperature, and whether melting is acceptable.
- Shortlist by molecular-weight range. Select liquid, semi-solid, or solid candidates based on required handling and end-use behavior.
- Review the supplier specification. Compare molecular-weight indication, viscosity or melting information, water content, appearance, and application-relevant purity controls.
- Run formulation-representative trials. Use the intended concentration, addition order, agitation method, and temperature profile.
- Inspect after equilibration. Evaluate clarity, phase separation, viscosity, crystallization, odor, color, and any change after cooling or storage.
- Confirm supply consistency. Ensure the ordered grade, packaging format, documentation, and change-control expectations are clear before qualification is finalized.
The final decision should state both the selected PEG grade and the reason it was selected. A useful approval note links the grade to measurable process needs: acceptable pumping temperature, required dissolution conditions, finished-formulation viscosity range, or melt behavior. That makes future sourcing discussions more precise and prevents a broad material name from being used as a substitute for an application-specific specification.
Send Us Your Inquiry Today
